Hydraulic Cylinder Final Inspection
Get An Instant QuoteFinal Inspection Steps

1. Re-measurement of Stroke, Mounting Center Distance, Clevis Center Distance and Thread Dimensions
For the first step of the final inspection, we re-measure the cylinder stroke, mounting center distance, clevis center distance and thread dimensions. First, while the cylinder extends and retracts back and forth, we take readings of its fully extended length and fully retracted length. Then we compare these values against the stroke tolerance range on the drawing to make sure the actual stroke meets drawing requirements. After measuring the stroke, we recheck the mounting center distance with the cylinder retracted and the clevis center distance with the cylinder fully extended. We also check the clevis pin hole diameter and the concentricity between the clevis pin hole and cylinder centerline. We make sure all dimensions match the drawing, so customers achieve precise alignment during on-site installation and avoid assembly jamming. After we finish checking the center distances, We use thread go and no-go gauges to check if the threads screw in properly, which lets us find any defects on the thread form.
corresponding steel heat number.
We record all measured values and compare them with drawing requirements to determine if each item passes or fails one by one. If any critical dimension is outside the drawing tolerance, we arrange rework or scrap the cylinder. For passed units, we keep complete test records rather than only marking them as qualified.
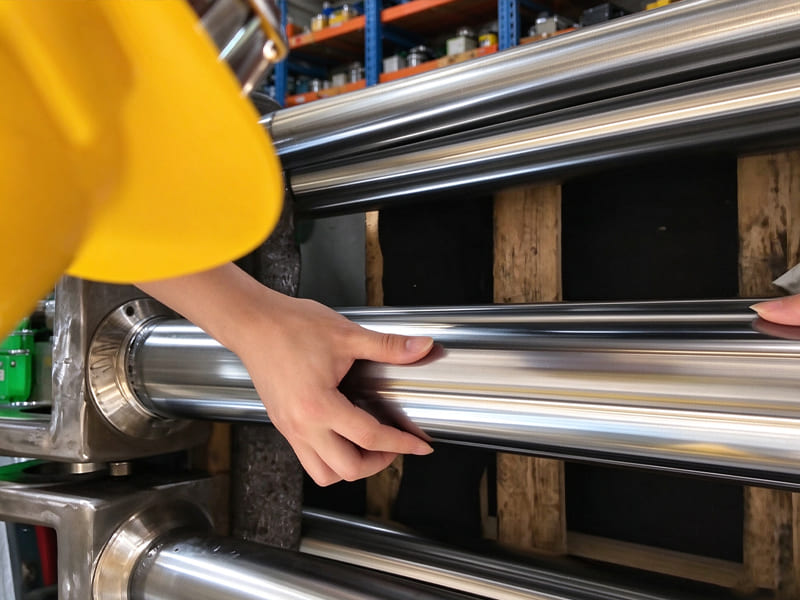
2. Visual Inspection of Paint Coating and Chrome-Plated Surface
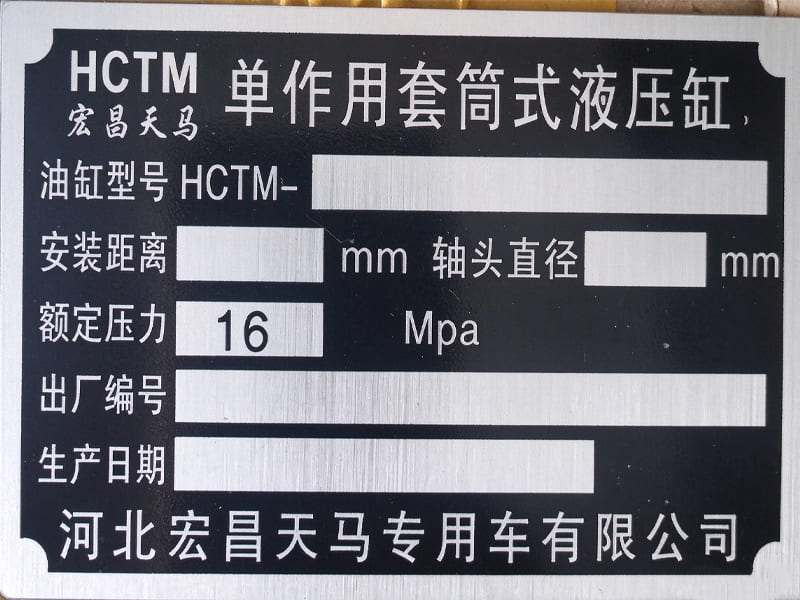
3. Nameplate Marking
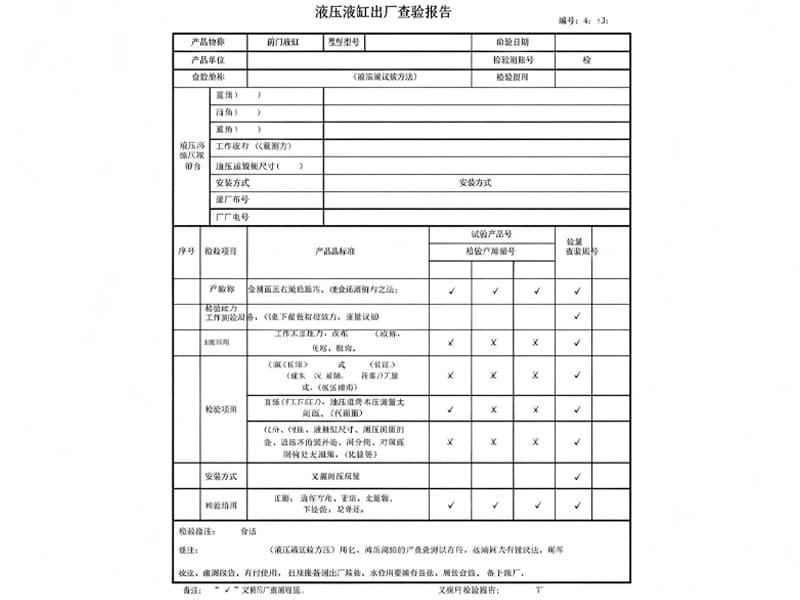
4. Technical Document Filing
Leveraging our full in‑house manufacturing capacity, we are ready to develop custom hydraulic cylinder solutions for your project. Please get in touch with us today.