Hydraulic Core Pull Cylinder Manufacturer
All cylinders undergo pressure testing before delivery.
MOQ starts from 1 piece, the lead time is 3 to 7 days.
We provide detailed quotations and technical support based on your mold drawings.
Brands We Serve in Hydraulic Industry
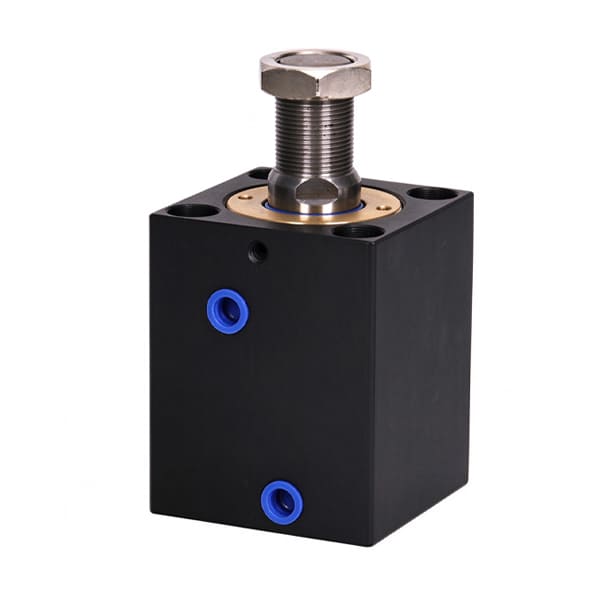
Hydraulic Core Pull Cylinder
Your Reliable Supplier of Hydraulic Core Pull Cylinder
Hydraulic Core Pull Cylinder


Applications of Hydraulic Core Pull Cylinder

Home Appliance Housing Injection Molding
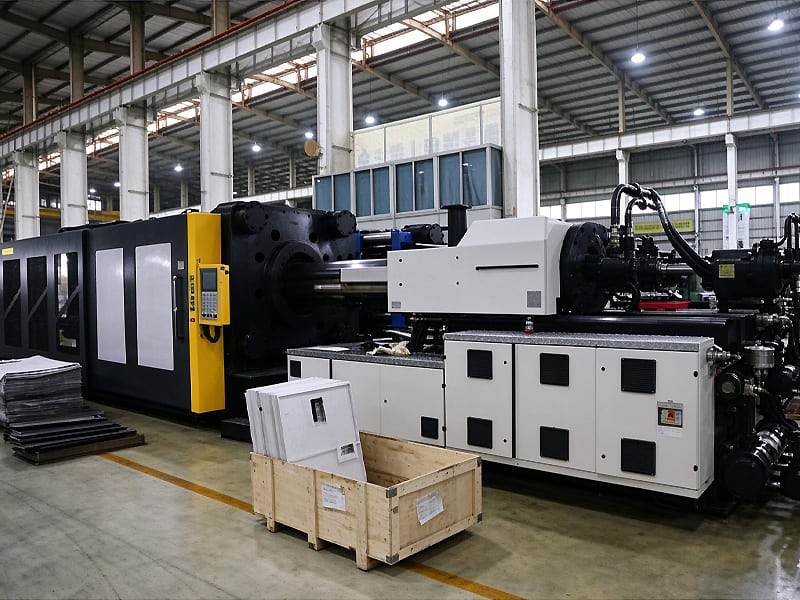
Automotive Exterior Injection Molding
Hydraulic core pulling cylinders are used in injection molds for automotive exterior parts.Before injection, the cylinder extends and drives the core into the mold cavity. After the part cools, the cylinder retracts and pulls the slide back to withdraw the side core, let the mold open and the part removed easily. The cylinder can be mounted in different positions and at different angles on the mold. It can do angled core pulling, rotary core pulling, and other movements, so it works well for complex parts.
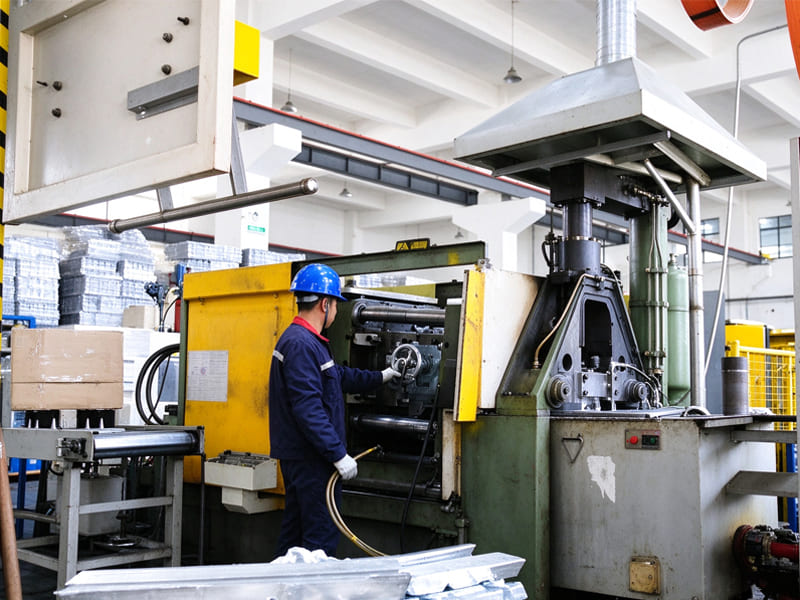
Aluminum Die Casting
Hydraulic core pulling cylinders are used in aluminum alloy die casting equipment. The cylinder drives the piston rod to push the slide, moving the core away from side grooves to finish core pulling. The hydraulic core-pulling cylinder can deliver a large pulling force in a short stroke, so it can easily pull the core out and avoid damaging the part surface.
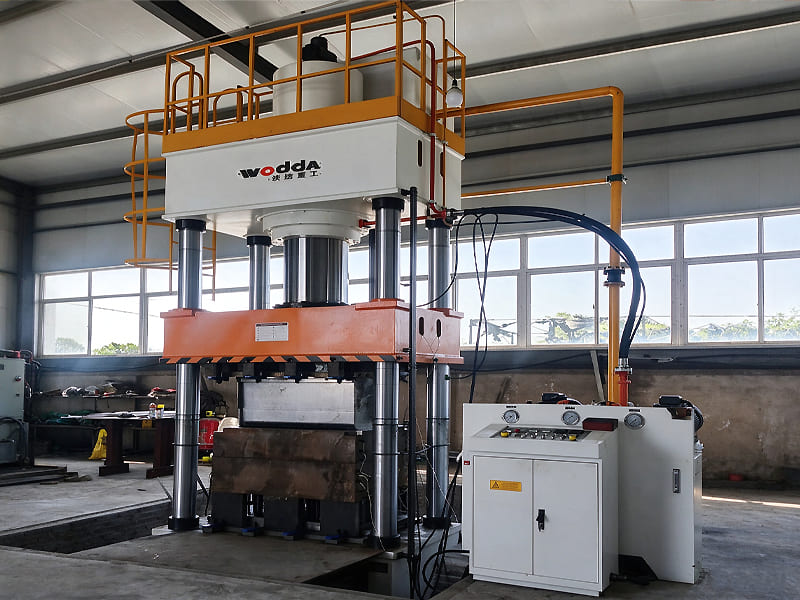
Compression molding
Hydraulic core pulling cylinders are used in compression molding equipment. The cylinder is mounted on the mold. It extends a piston rod that connected to the sleeve pin pressure block, pushing the sleeve pin forward into place for work piece molding. We fit a high-strength mold heat insulation plate between the cylinder and mold. It can block heat transferred from the mold and keeps the cylinder working steadily.
Insert locating
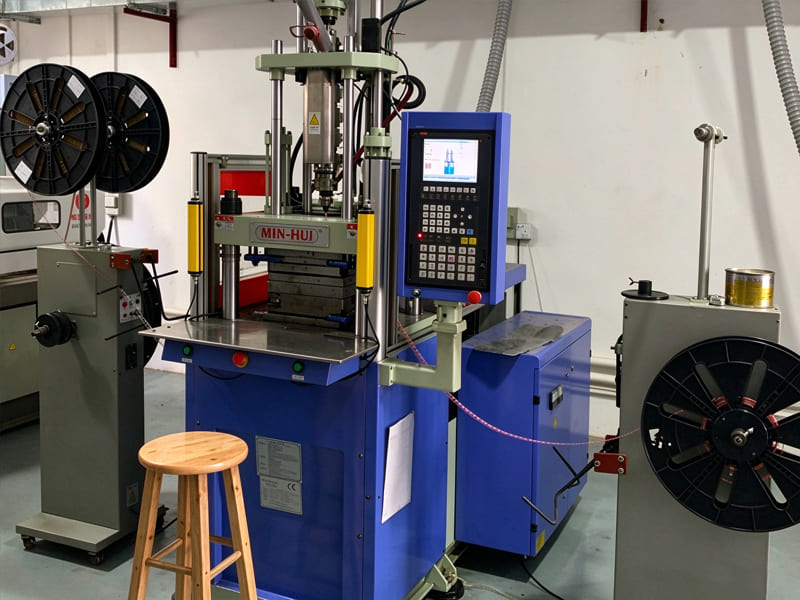
Hydraulic core pulling cylinders are used in insert positioning equipment. The cylinder drives the slide to press the insert tightly and hold it firmly in the set position for later processing.The cylinder provides steady and reliable clamping force to fix the insert securely. The insert will not easily shift or move during injection molding.

Multi-Cavity Mold Injection Molding
Hydraulic core-pulling cylinders are used in multi-cavity injection molding equipment. The piston rod pushes the outer slide, and the slide pulls the molding cores through a linkage at the same time. This let one cylinder can drive several cores to pull together. The hydraulic system can send hydraulic oil evenly to each core-pulling cylinder, so the core-pulling actions in all molds stay in sync.
Core back under injection pressure
After the cylinder pulls the core into place, it need a hydraulic lock to hold position. If the hydraulic lock has internal leakage, its locking force will weak. Injection molding or die casting will create a high-pressure back force, so when the hydraulic system loses pressure, the weakened hydraulic lock cannot hold the core, and the core will move back. The position becomes unstable, and the product deforms.
We add a mechanical locking mechanism to the cylinder. When core pulling finishes, a mechanical pin locks the piston rod. The position no depends on hydraulic pressure. Even if the hydraulic lock leaks or the system loses pressure, the mechanical structure still locks the core firmly. It can resist the high-pressure back force from injection, keeps the core from moving back, and prevents product deformation.

Pressure cannot be released
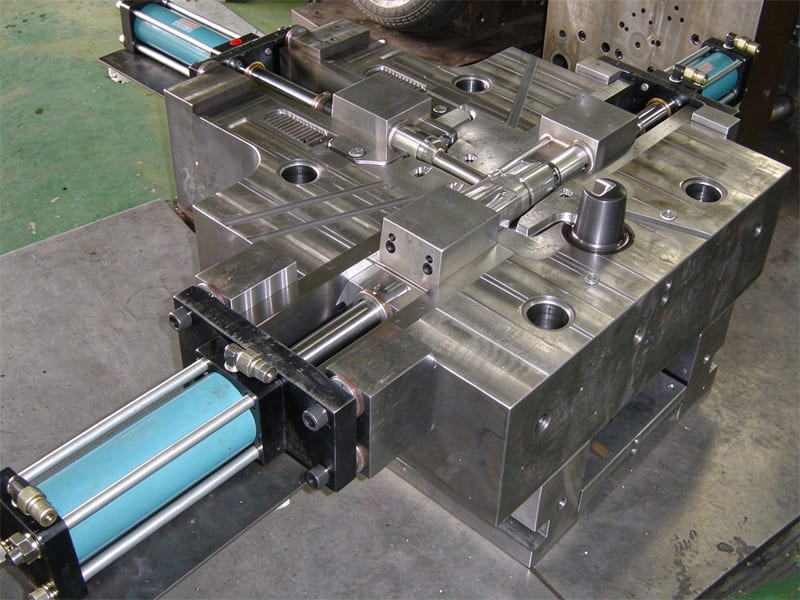
After the core is pulled into place, it need to keep high pressure to keep it locked so the melt can’t push it back. Once locked, both cylinder chambers are closed. If the pilot-operated check valve’s opening pressure is too low, or the pilot oil line is blocked, oil will be trapped inside the cylinder during unlocking. The hydraulic pressure can’t release, and the high pressure presses the check valve spool tight, so the valve cannot open and the core cannot retract.
We fit a small pre-relief valve before the pilot check valve. When unlocking, this relief valve opens first to release the high pressure on the spool. Then open the pilot check valve, this way, the valve won’t get stuck by high pressure, and the cylinder can pull the core smoothly. We also enlarge the pilot tubing to prevent insufficient flow, This ensures enough oil pressure to open the valve during unlocking.
Position accuracy insufficient
Traditional hydraulic core-pulling cylinders didn’t have position feedback. The system only sends oil commands, so it can’t monitor or correct the cylinder position in real time. When internal leakage, oil temperature changes, or other issues cause position deviation, it can’t correct automatically. This cause cylinder positioning accuracy is only ±0.1 mm. It can’t meet the ±0.02–0.05 mm positioning requirement for precision molds. It makes product dimensions unstable.
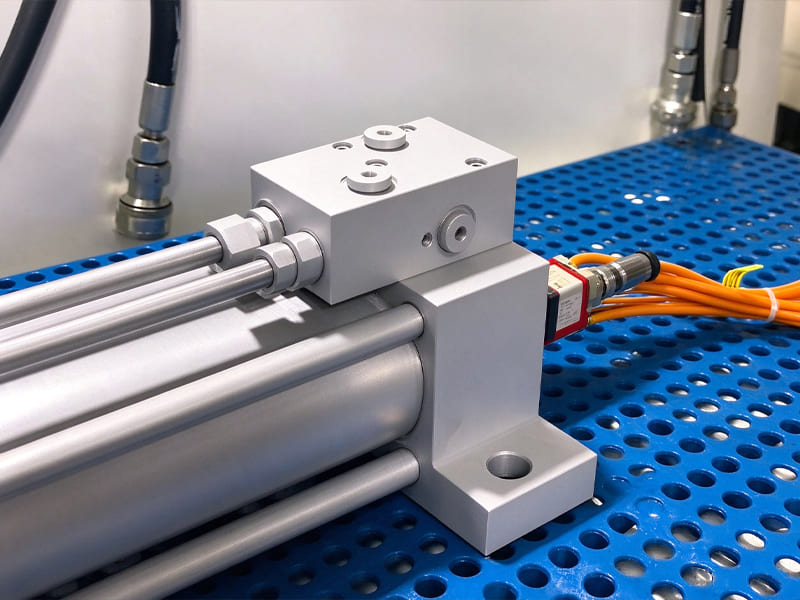
We install a position sensor inside the cylinder and use a closed-loop proportional hydraulic system. This can feed the piston rod position back to the controller in real time. When the position shifts, it automatically adjusts the cylinder position. It improves the repeat positioning accuracy to ±0.01~0.02 mm, meeting the positioning needs of precision molds.
Certifications
REACH Certificate
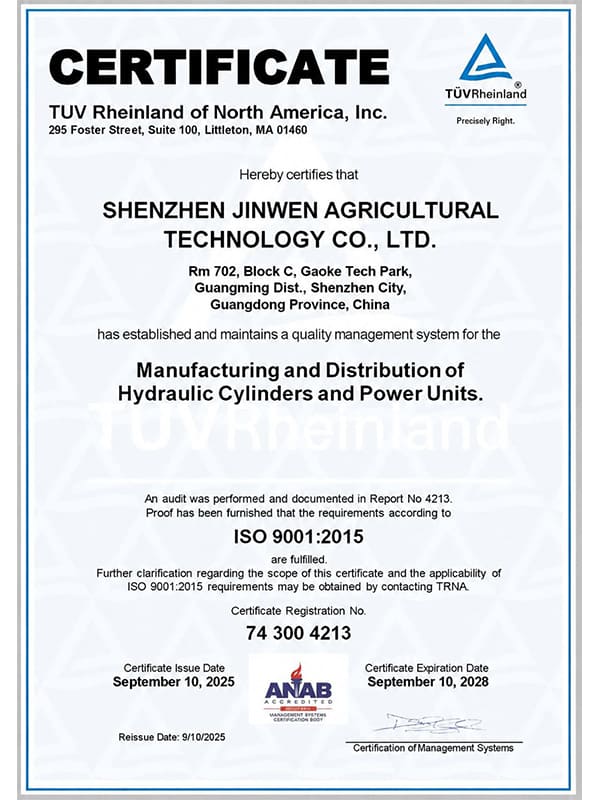
ISO 9001 Certificate
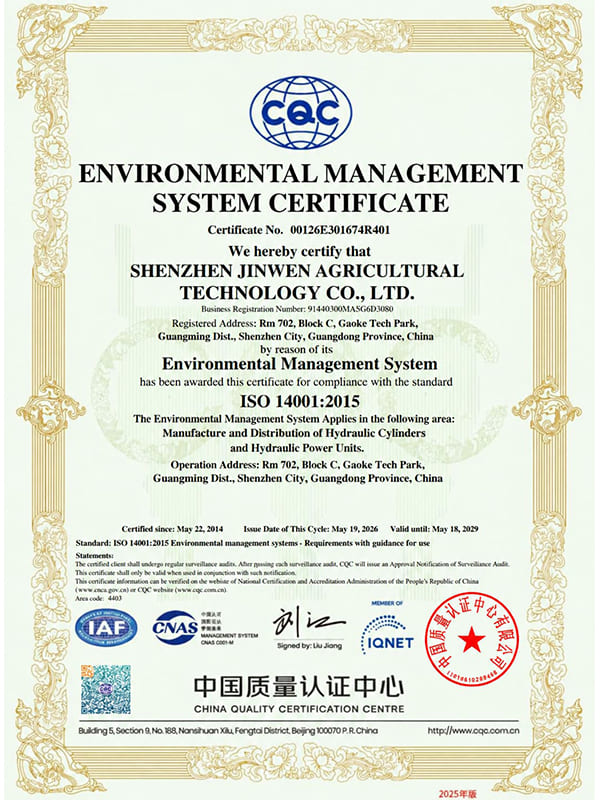
ISO 14001 Certificate
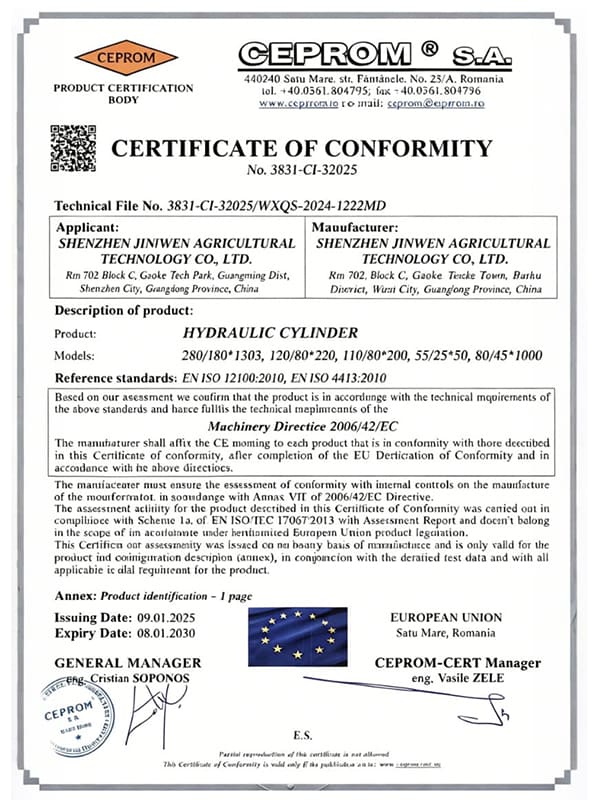
Certificate of Conformity
Why Work with Us
Safety Mechanical Locking
Using a dedicated mechanical self-locking structure, the hydraulic system can relieve pressure for standby and reduce equipment energy consumption.
After-sales Support
you can send us photos and videos if have problem, we will analyze them and quickly provide solutions to save your waiting time.
High Temperature Resistance
The sealing components use FFKM , it can withstands continuous temperatures of about 260°C and enables stable work in high-temperature environments.
Easy Maintenance
We optimize sensor mounting structure uses a split-type quick-install base, greatly shortening maintenance time.
How to Customize Your Hydraulic Core Pull Cylinder
Send Your Drawing
Provide us the detailed drawing or physical sample or critical dimensions, working pressure, mounting details.
Working Environment
Whether the cylinders works in high temperature, humidity, salt spray, dust and high frequency, pressure.
Get Quick Quote
We review all details of drawing and requirements and provide optimization suggestions with our experiences if necessary.
Production Procedure
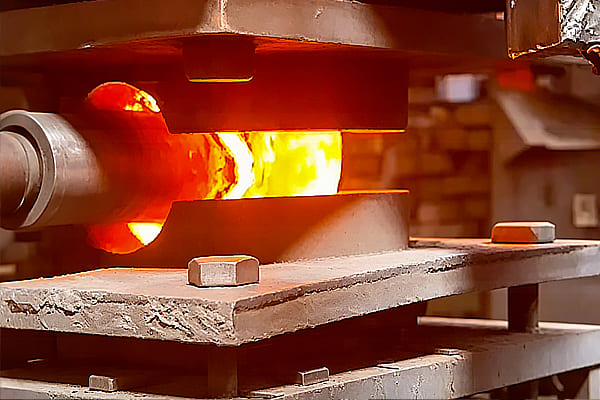
Integral forging
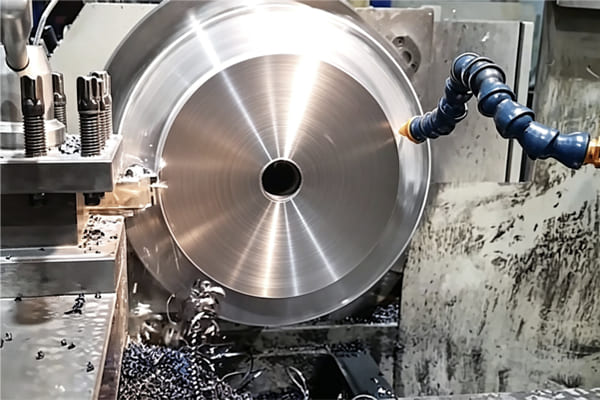
Turning
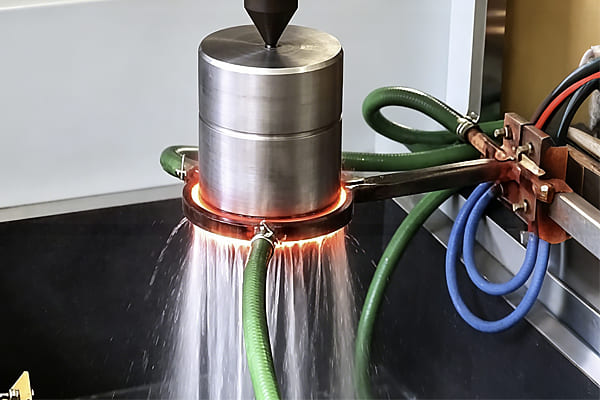
Induction hardening
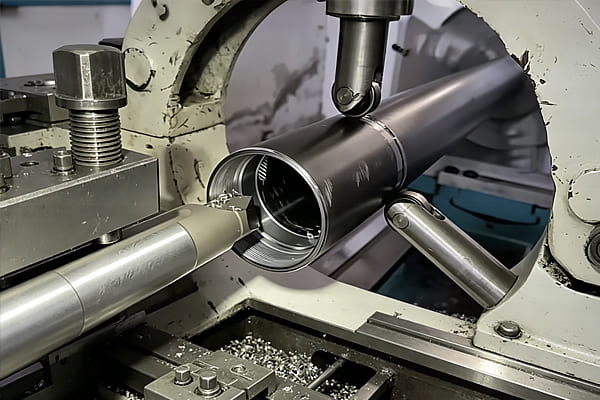
Cylinder barrel turning
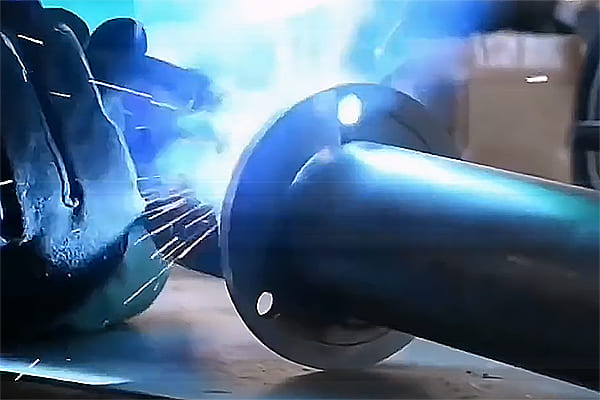
Welding
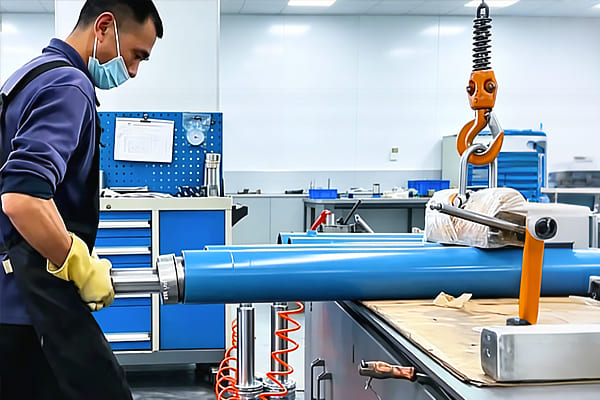
Assembly
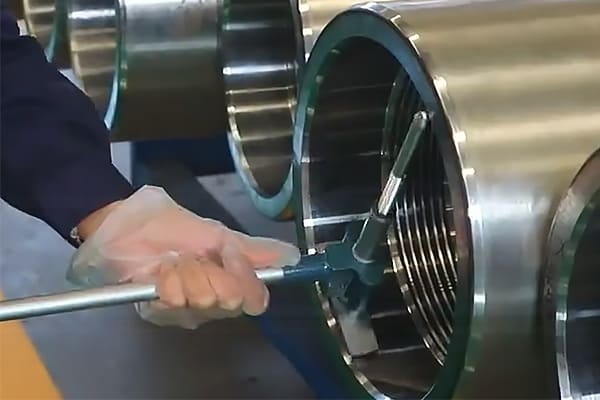
Dimensional measurement
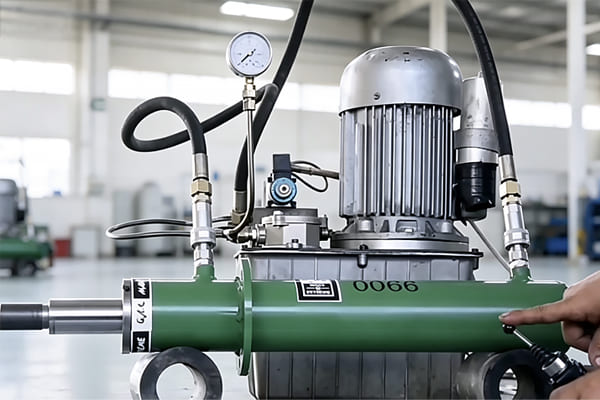
Pressure test