Excavator Hydraulic Cylinders Manufacturer
Our Excavator hydraulic cylinders are 100% tested under 1.5 times rated pressure.
MOQ starts from only 1 piece.
Send us your drawings or specs for an engineering review and quote.
Brands We Serve in Hydraulic Industry
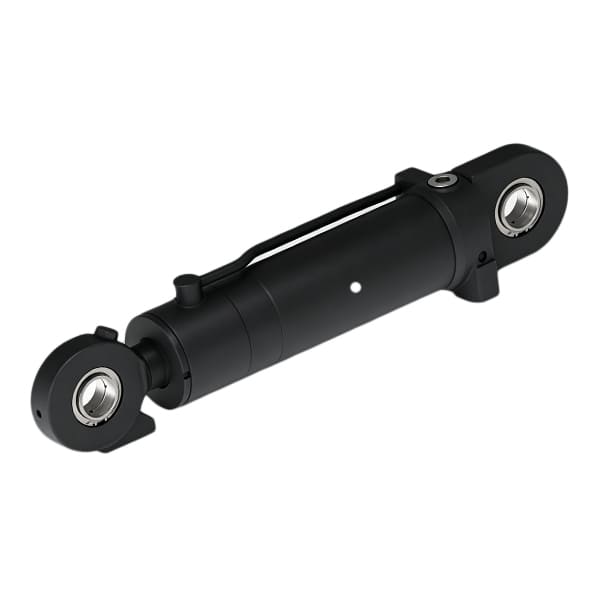
Excavator Hydraulic Cylinders
Your Reliable Supplier of Excavator Hydraulic Cylinders
Excavator Hydraulic Cylinders
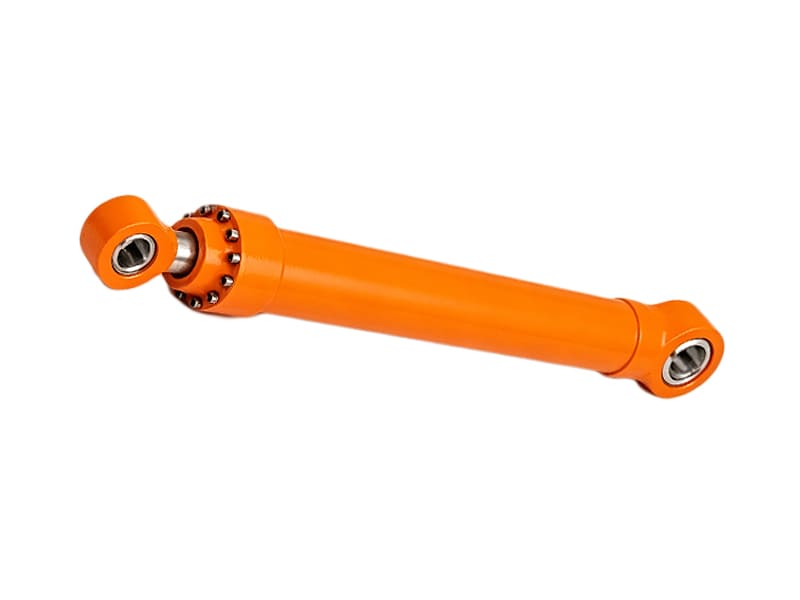
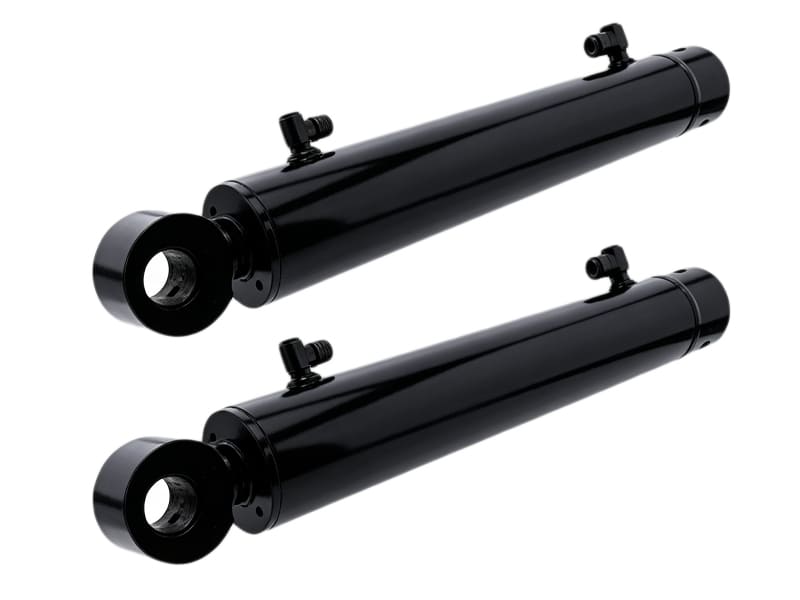
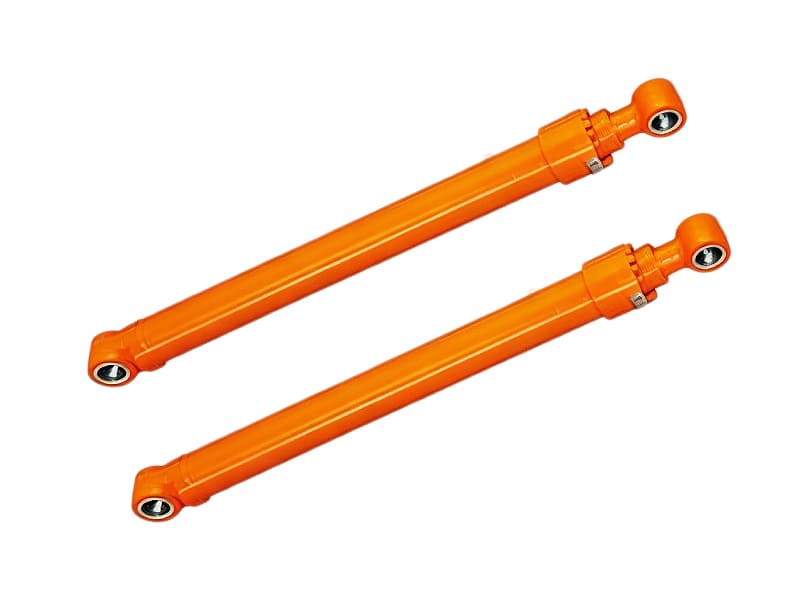
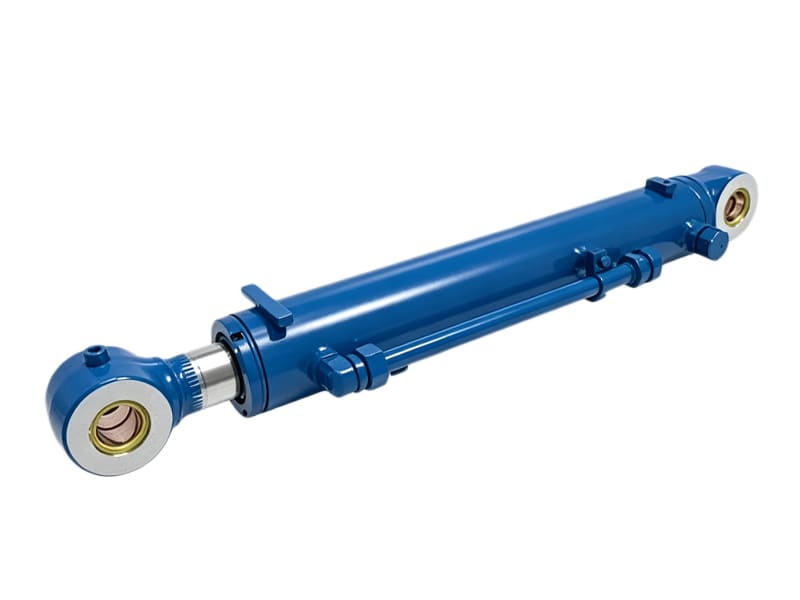
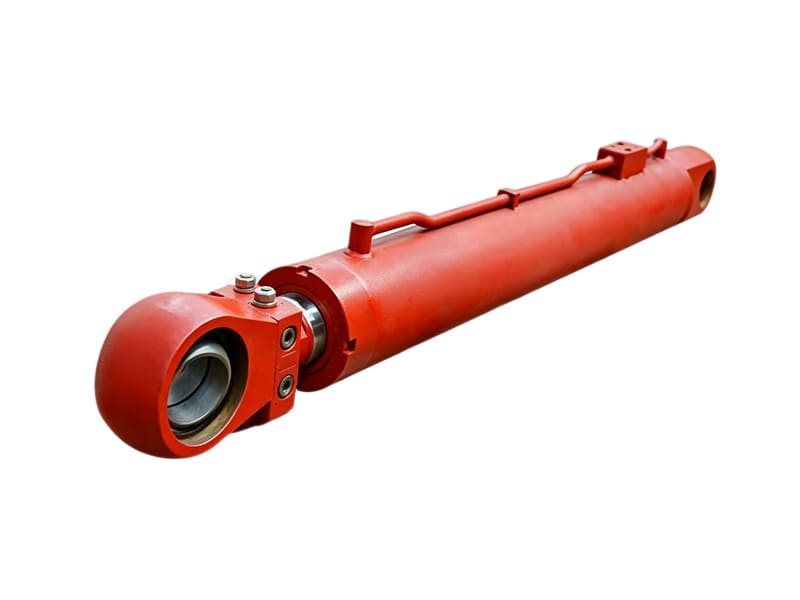
Applications of Excavator Hydraulic Cylinders
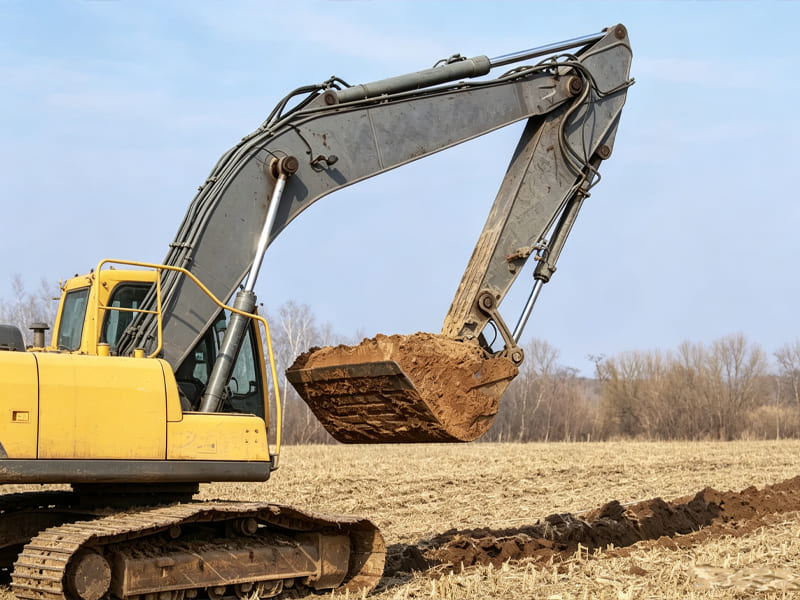
Boom Operation
The boom cylinder on an excavator powers the boom to lift and lower. This application demands high thrust from the cylinder. For a 20-ton-class excavator, its boom cylinder normally has a 140 mm bore. It works at up to 35 MPa, so a single unit can put out 35-40 tons of thrust to move the boom, steadily lifting the bucket and loads.
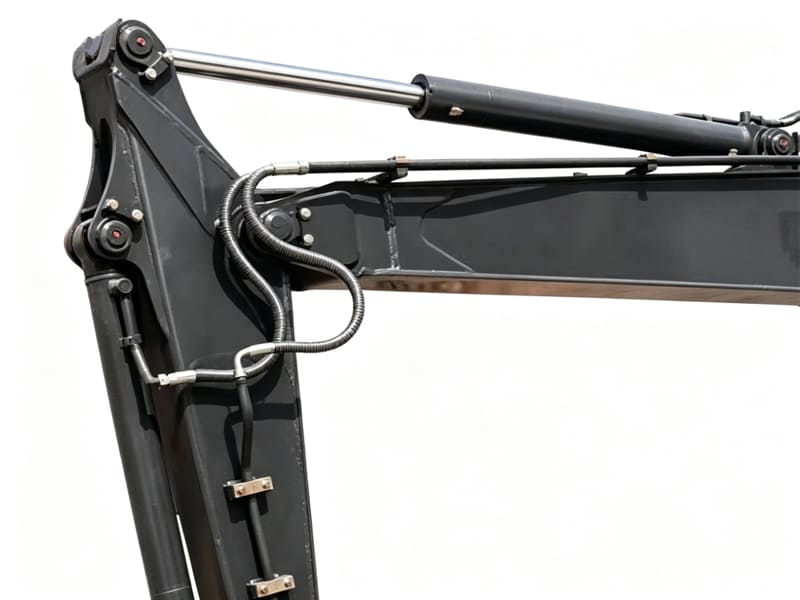
Arm/Stick Operation
The stick cylinder on an excavator powers the stick, which moves the bucket forward and down, then pulls it back and up for digging and grading. This digging process creates large side-forces, so this application demands strong resistance to side-loading from the cylinder. For our excavator cylinders, we keep the guide sleeve fitting clearance within 0.02-0.04 mm. This closely-controlled tolerance prevents the piston rod from scoring the inner barrel surface.
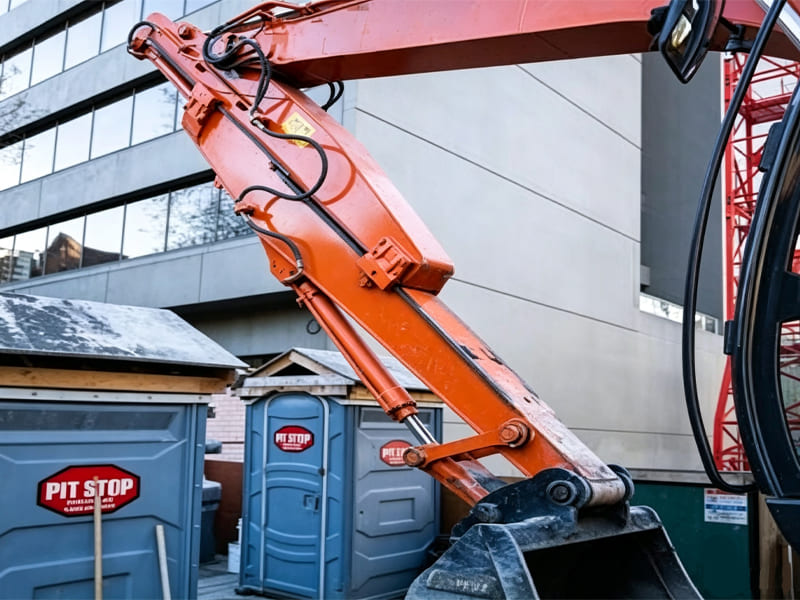
Bucket Curling/Dumping
The bucket cylinder on an excavator powers the bucket to tilt and curl in and out. Mounted at the far end of the working attachment, this cylinder sees repeated sudden internal high-pressure shocks when the bucket cuts into soil and rock. Its peak internal pressure can hit 1.2-1.5 times the cylinder’s rated pressure, so this application demands strong resistance to sudden high-pressure shocks. Our cylinder barrel wall stands up to repeated shock loads above 40 MPa. We also hold H7/f7 fit between the barrel bore and guide sleeve to avoid piston rod scoring under shock conditions.
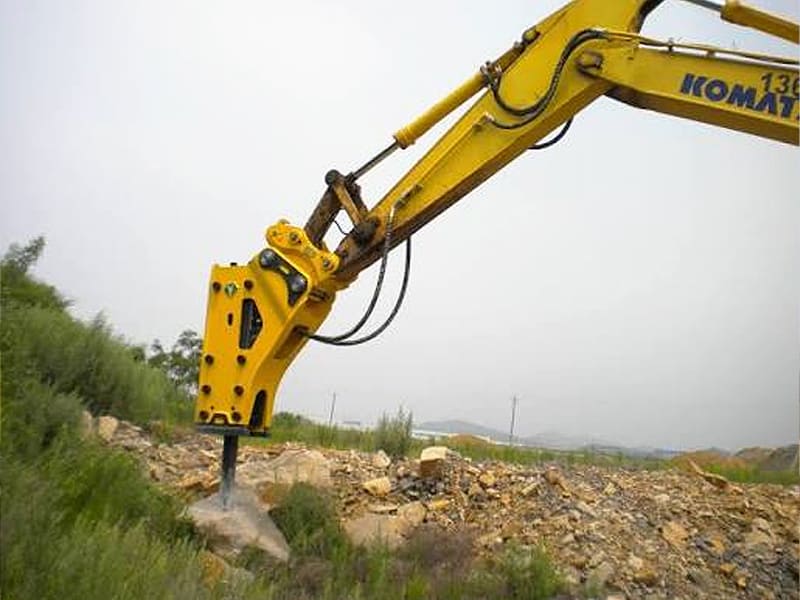
Demolition & Breaker Duty
The bucket cylinder on an excavator powers the breaker for positioning, pressure-driven feed and hammer lift. This application demands high-level resistance to high-frequency vibration. For our bucket cylinder ports, we offer wire-thread anti-loosening inserts or double-nut locking structures. Both stop fittings from coming loose under continuous vibration.
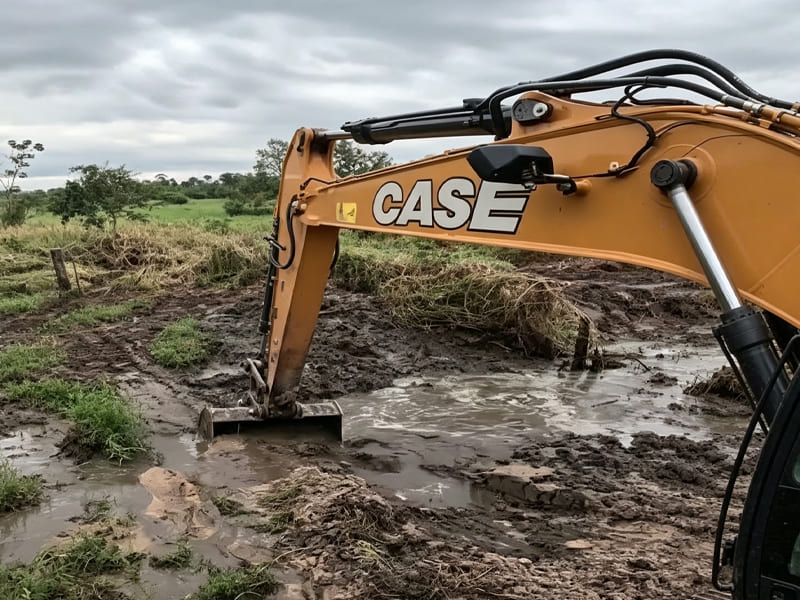
Amphibious & Drainage Trenching
The excavator boom and arm cylinders work together to power buckets and dredging attachments for underwater positioning and silt removal. This application demands high resistance to hydrolytic ageing for cylinder seals. These cylinders’ guide sleeves carry a polyurethane double-lip dust wiper to keep sand and grit out of the cylinders.
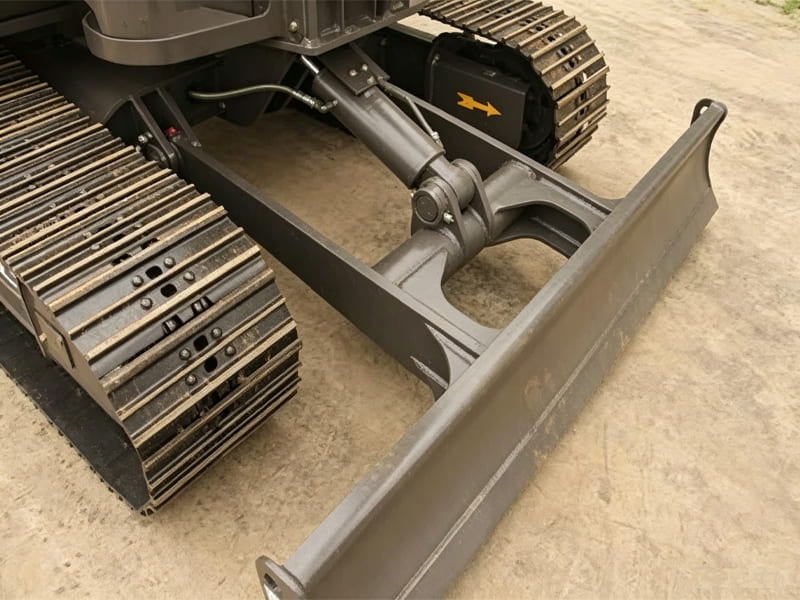
Outrigger & Blade System
The outrigger and dozer-blade cylinders work together to power the outrigger pads and front dozer blade to perform machine jack-up, blade angle adjustment and blade raise-and-lower operations. These applications demand high cylinder performance against internal leakage during pressure-holding. Our outrigger-cylinder pistons are fitted with Glyd-ring primary seals, polyurethane secondary seals and nylon backup rings. This reduces inherent risks of cylinder internal leakage.
Dust-Driven Wear and Seizure on Excavator Hydraulic Cylinders
Cylinder wear and seizure are common failures on excavator hydraulic cylinders. Excavators work at job sites with heavy sand and dust, where piston rods remain exposed over long operating periods. Sand and dust are drawn into the cylinder barrel as the rod extends and retracts. These hard particles act as abrasives: they scratch the inner barrel surface and speed up component wear. When particles accumulate within the clearance between piston and barrel, they can cause direct cylinder seizure.
We closely control piston-rod machining. Our surface roughness stays at Ra 0.2-0.4 μm, with chrome-plating thickness of 15-25 μm and surface hardness reaching HV 700-1150. This reduces dust-particle adhesion and lowers the risk of contaminants being drawn into the cylinder.
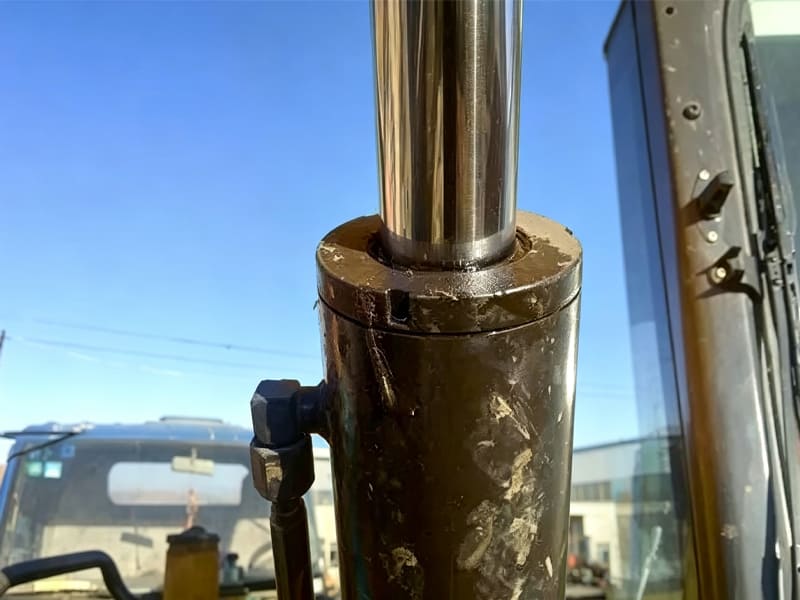
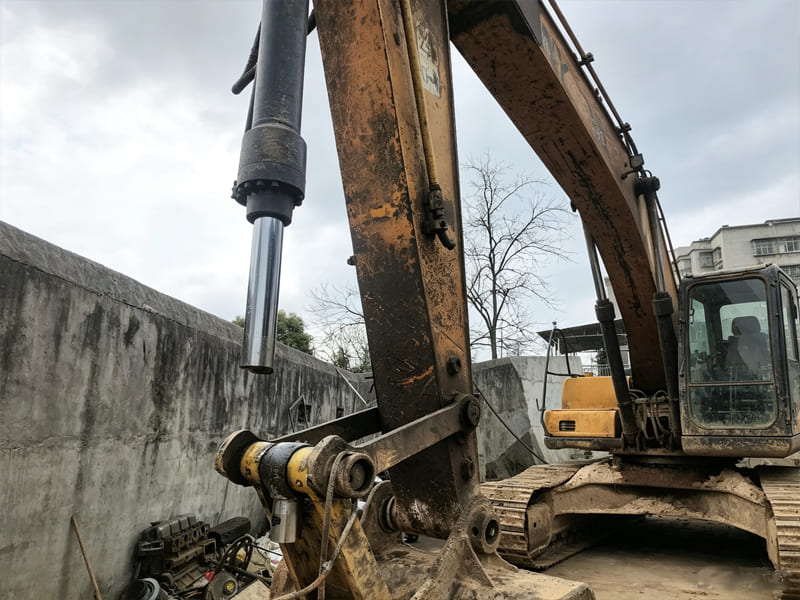
Piston Rod Mechanical Damage and Fracture on Excavator Hydraulic Cylinders
Piston-rod mechanical damage and breakage are common failures on excavator hydraulic cylinders. Flying rock fragments can hit at speeds over 20 m/s during excavator operation. When they strike the chrome-plated piston-rod surface, they may leave dents 0.2-0.5 mm deep. These damaged spots create stress concentrations. As the piston rod extends and retracts repeatedly, cracks form at these dents and keep propagating.
We source raw cylinder steel strictly to material grades specified on customer drawings and re-check the chemical composition of every incoming batch of round steel, keeping harmful impurities such as sulphur and phosphorus at low levels. These impurities stay below 0.015 % for sulphur and 0.020 % for phosphorus. This improves steel toughness, giving our piston rods solid fatigue resistance. Besides, we quench and temper our piston rods. Quenching temperature runs 840-860 °C, and tempering temperature runs 560-600 °C. We hold heat for at least one hour for every 25 mm of piston-rod section thickness, delivering base-metal hardness of HB 220-260. We also target a hardness gap between core and surface no higher than HB 30. This avoids low-strength spots forming on the piston rod.
Cushioning Failure Triggering Hydraulic Impact on Excavator Hydraulic Cylinders
Buffer failure is a common issue for excavator hydraulic cylinders and causes heavy impact at stroke end. This is mostly caused by poorly designed annular clearance between the buffer plunger and buffer sleeve, which produces either excessive or insufficient pressure drop across the buffer throttle. When pressure drop becomes excessive, instant shock pressure inside the cylinder can reach 2.5 to 3 times the cylinder’s rated working pressure. High-pressure shock waves pass through hydraulic oil and act directly on the cylinder bottom and piston. The cylinder produces loud banging noise as the piston reaches the end of its stroke.
Take the standard 0.03-0.08 mm clearance from customer drawings as an example. Following these given tolerances, we set the mating clearance between buffer plunger and buffer sleeve close to the mid-point of this range, around 0.055 mm, and keep clearance variation within 0.02 mm. As oil flows through the gap between buffer plunger and buffer sleeve, pressure-response and buffer deceleration follow drawing specifications. This reduces shock pressure at the end of the stroke and brings down banging noise, protecting the cylinder bottom and seals from impact damage.
Certifications
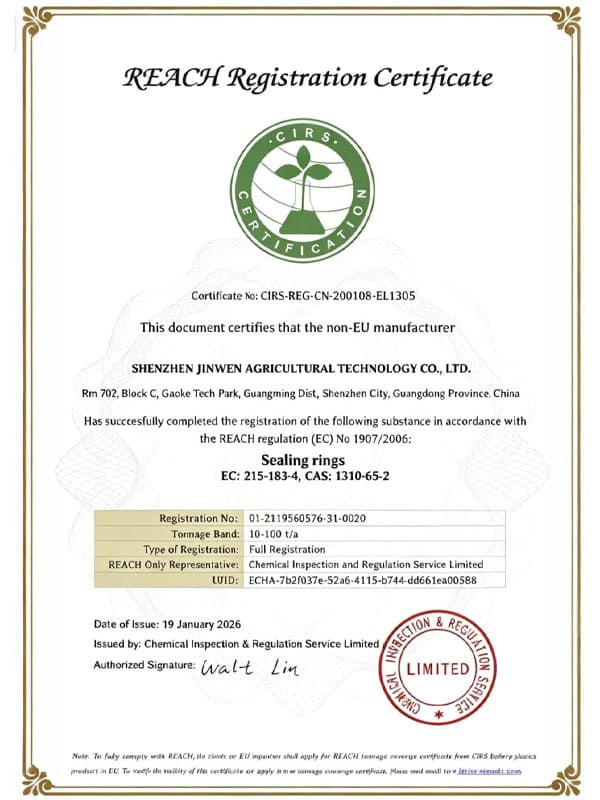
REACH Certificate
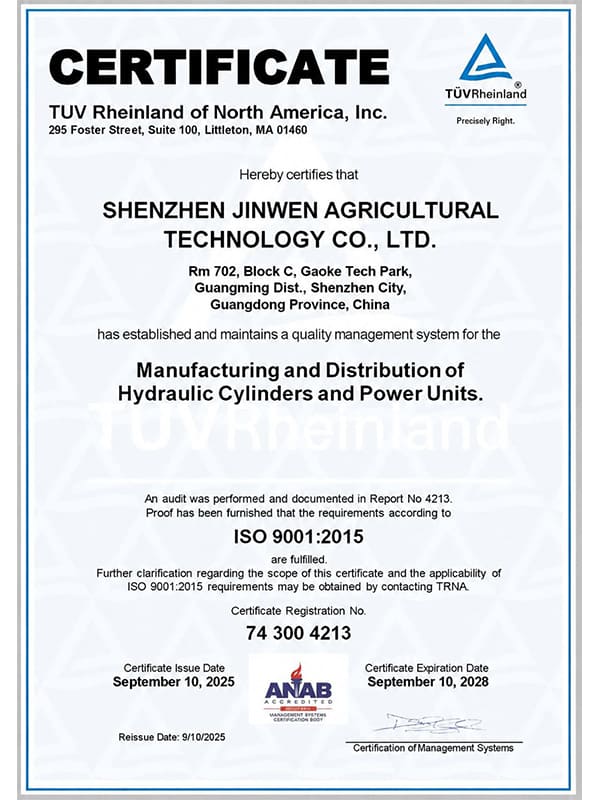
ISO 9001 Certificate
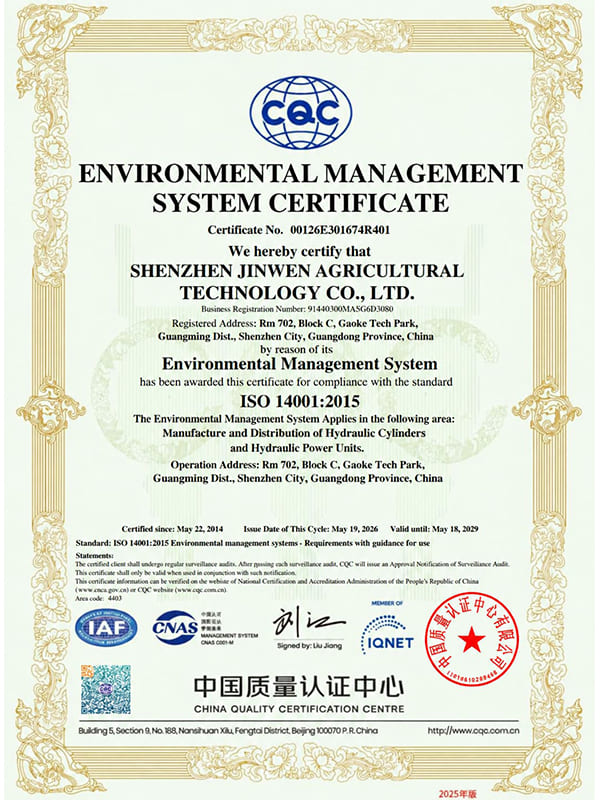
ISO 14001 Certificate
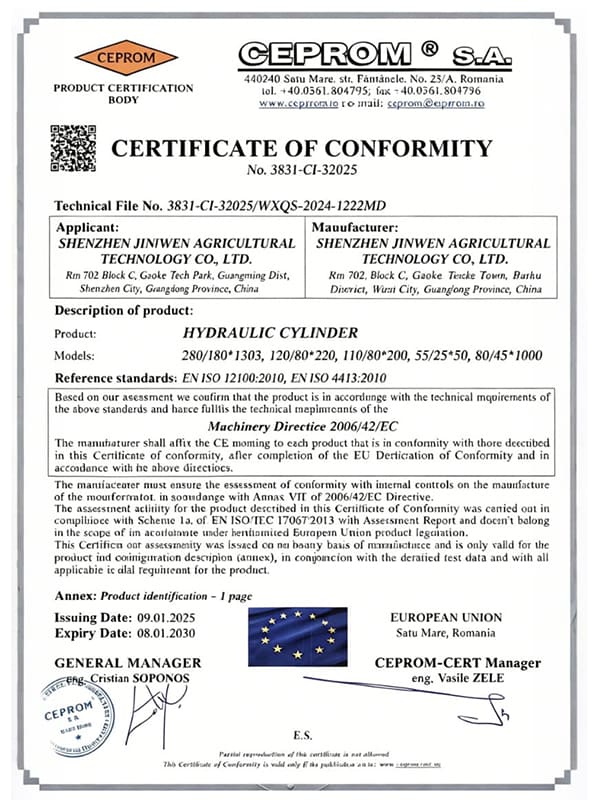
Certificate of Conformity
Why Work with Us
Full-Stroke Load Testing Before Shipment
Before shipment, we run full-stroke loaded tests for every excavator hydraulic cylinder on the test bench.
End-to-End In-House Manufacturing
We carry out all processes for our excavator hydraulic cylinders, including cutting, forging and assembly, at our own factory for consistent product quality.
Seamless OEM Dimensional Replacement
We can manufacture excavator hydraulic cylinders according to your drawings, with mounting interfaces that fit your equipment for direct drop-in replacement.
Preventive Seal Replacement Guidance
We include a seal replacement guide card with every shipment, listing recommended seal inspection intervals and early signs that seals need replacing.
How to Customize Your Excavator Hydraulic Cylinders
Send Your Drawing
Provide us the detailed drawing or physical sample or critical dimensions, working pressure, mounting details.
Working Environment
Whether the cylinders works in high temperature, humidity, salt spray, dust and high frequency, pressure.
Get Quick Quote
We review all details of drawing and requirements and provide optimization suggestions with our experiences if necessary.
Production Procedure
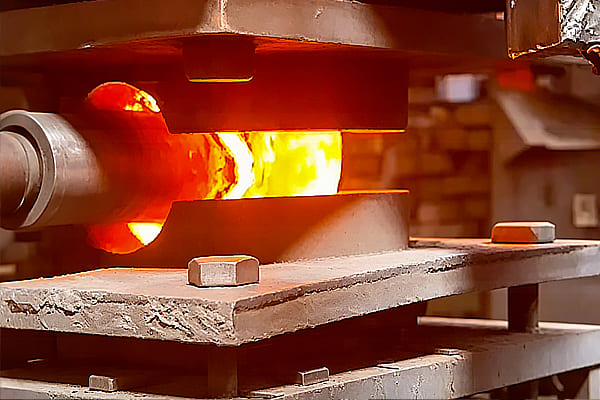
Integral forging
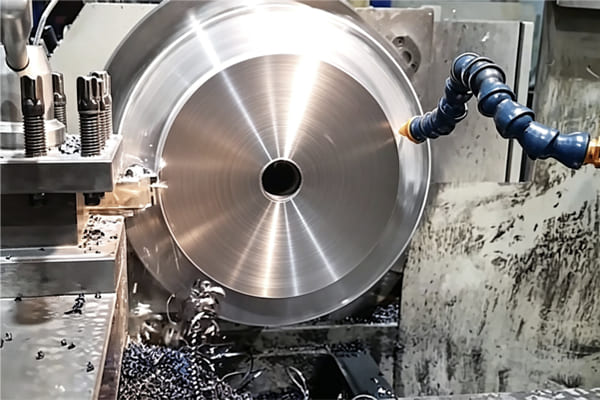
Turning
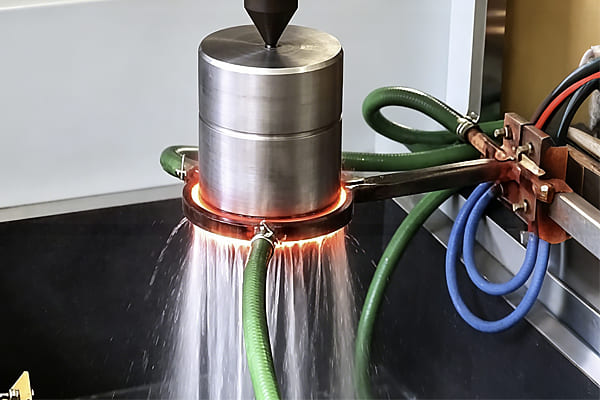
Induction hardening
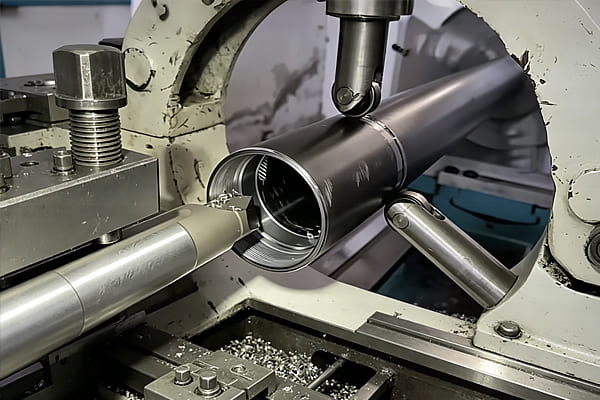
Cylinder barrel turning
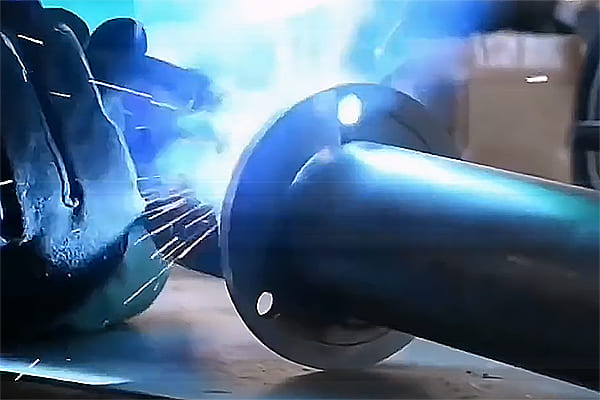
Welding
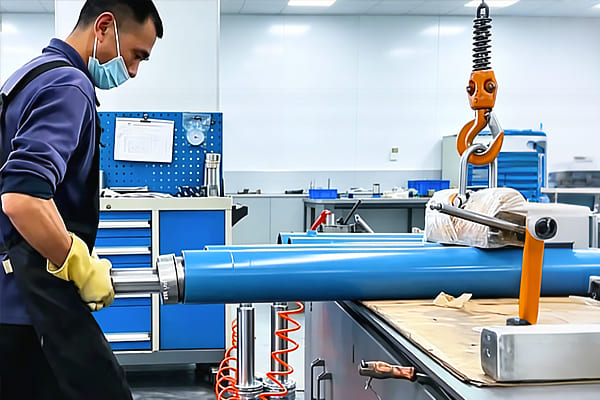
Assembly
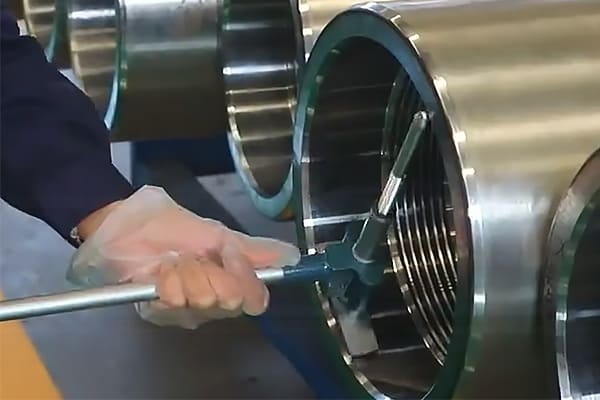
Dimensional measurement
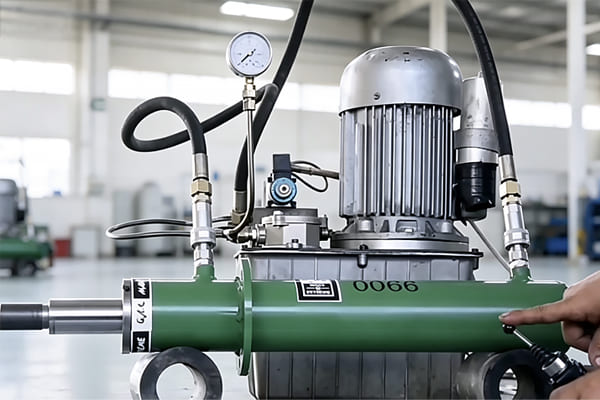
Pressure test